Forging closer to the final shape saves material, machining time and tool wear — but only if dimensional consistency is real, not nominal.
2026-08-05 · معرفة التروس
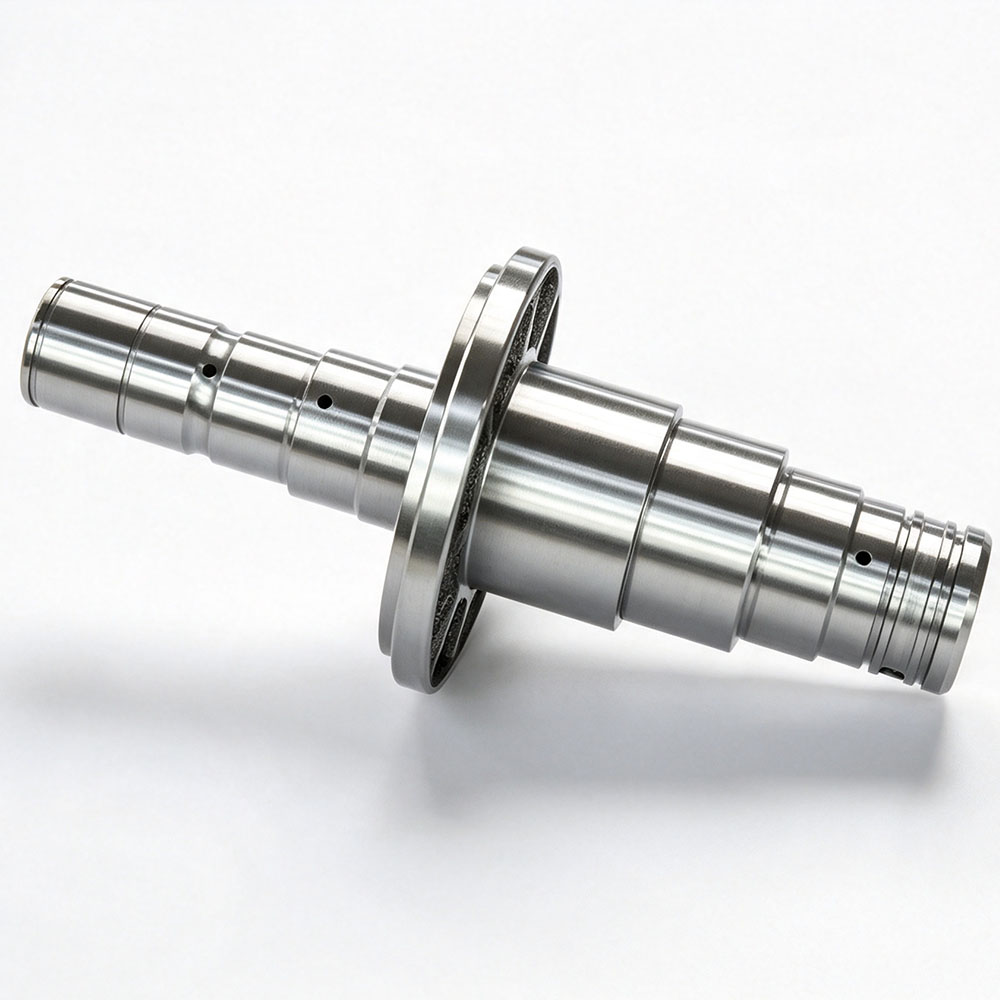
A gear blank bought as a near-net forging costs more per kilogram than a sawn bar. It still lowers total cost, because it removes three expenses that are easy to miss: material loss in the bore and web, roughing time on a CNC lathe, and the tool wear that comes with interrupted cuts through scale.
The saving depends entirely on how close the forging really is. If the bore is forged within a millimetre and the web thickness within half a millimetre, the machining program can take one clean pass instead of three, and the chip load drops by 15–25% of blank weight. If the forging varies batch to batch, the programmer has to protect against the worst case, and most of the benefit disappears.
Grain flow is the second reason. A forged blank has fibres that follow the component's contour; a bar-cut blank has fibres running straight through and out of the surface at the tooth root. Under bending fatigue the difference is measurable — our own precision-forged gears are specified at about 20% higher strength than the equivalent cut-from-bar part.
When you evaluate a blank supplier, ask for the dimensional capability study rather than the tolerance table, and ask which dimensions are forged and which are machined. A supplier who forges the bore and the web and leaves only the teeth to be cut is usually the one whose blank actually pays for itself.